صيانة قوالب الأنابيب الخرسانية الجاهزة: محاذاة حلقات النهاية، واختيار مواد فك القالب، والفك الدقيق
إطالة عمر القالب ليتجاوز 10,000 دورة صب مع إعادة ضبط الحلقات بالمخرطة وصيانة الخوابير وموانع الالتصاق.
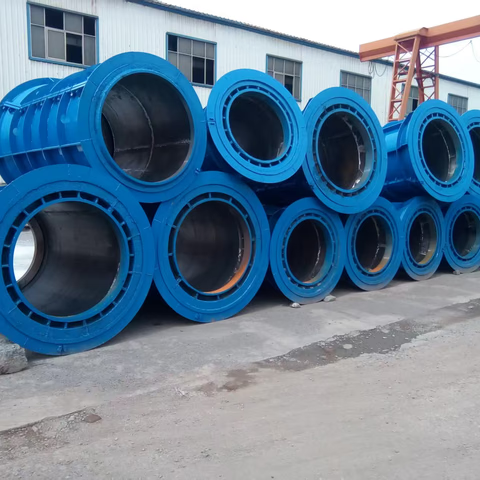
تمثل قوالب الصلب استثماراً رئيسياً في المصنع. حافظ على دائرية المفصل ضمن ±0.5 مم وامنع التفتت السطحي باستخدام قائمة التحقق المنتظمة ودليل استخدام زيوت فك القوالب المتطورة.
1. The Value of Mold Maintenance
Heavy steel concrete pipe molds endure severe operational stresses: intense mechanical roller compaction, thermal expansion cycles from 20掳C to 75掳C, abrasive aggregate wear, and crane handling. Without structured daily maintenance, molds suffer joint warping, out-of-round deformation, and slurry leakage at the bell and spigot joints.
Well-maintained Q345B steel molds fabricated by HLY routinely deliver 10,000+ casting cycles over a decade of operation when following standard maintenance procedures.
2. Daily Cleaning Protocols Without Hammer Damage
- No Sledgehammer Abuse: The most common cause of deformed molds on plant floors is workers striking the steel skin with heavy sledgehammers to dislodge adhered mortar. Even a 2 mm localized dent creates an out-of-round pipe section. Always use pneumatic scrapers, brass chisels, or high-pressure washers.
- Joint Groove Descaling: Scrape all hardened mortar residue from the tongue-and-groove joint channels, edge ring seating lips, and bolt holes immediately upon de-molding while the residue is still warm.
- Flange Flatness Check: Inspect longitudinal mating flanges for dried slurry buildup. Gaps between mating faces allow pressurized water-cement slurry to bleed out, resulting in honeycombed exterior pipe seams.
3. Release Agent Chemistry & Application Ratios
Avoid using raw used motor oil or diesel fuel on mold interiors. Raw oils cause severe surface staining, air-bubble entrapment (bugholes), and degrade rubber joint seals over time.
Recommended Formulations:
鈥?Summer Formulation: Premium water-in-oil emulsified release agent (emulsifier : clean water = 1 : 10). Uniformly atomized using low-pressure spray wands.
鈥?Winter Formulation: Emulsified release agent heated with low-pressure steam to 40掳C before spraying to prevent viscous agglomeration on cold steel plates.
鈥?Fasteners & Edge Rings: Apply clean mineral oil or silicone paste on connecting bolts and alignment pins to facilitate rapid pneumatic tightening and disassembly.
4. End-Ring Precision & Jacking Pipe Tolerances
For microtunneling trenchless jacking pipes (椤剁), the end rings of the mold dictate the squareness and planarity of the pipe bearing faces. If the end face is out-of-square by even 1.0 mm, jacking thrust loads (often exceeding 1,500 kN to 5,000 kN) will concentrate unevenly during tunneling, causing catastrophic pipe shattering underground.
HLY precision end rings are forged from heavy alloy steel and CNC-lathed on our 8-meter horizontal lathes to within 卤0.5 mm perpendicularity tolerance. Plant maintenance teams must inspect end rings monthly with precision dial gauges and surface flatness straightedges.
5. Longitudinal Flange & Fastener Management
Always tighten longitudinal connecting bolts symmetrically from the center of the mold outward toward both ends. Uneven tightening pulls the cylindrical shell into a slight corkscrew twist, leading to longitudinal pipe cracking during the heating stage of steam curing.
6. Long-Term Storage & Anti-Corrosion Preservation
When molds are removed from active rotation for size changeovers or seasonal shutdowns, store them horizontally on level timber dunnage in a dry covered yard. Coat all bare internal working surfaces with a heavy rust-preventative oil (闃查攬娌? to eliminate atmospheric pitting.
Planning a Concrete Pipe Manufacturing Project?
Our engineering team provides comprehensive turnkey plant calculations, foundation layout drawings, mold customization specifications, and commercial quotations within 2 hours.
مقالات فنية ذات صلة
نظام المعالجة بالبخار للأنابيب الخرسانية: بروتوكول حراري من 4 مراحل للأنابيب عالية المقاومة
تعمل المعالجة بالبخار على تسريع اكتساب الأنابيب لمقاومة الضغط للشحن السريع. اتبع جدولنا الحراري المكون من 4 مراحل لتحقيق مقاومة C35–C50 خلال 8 ساعات مع منع الشقوق الدقيقة.
لوجستيات ساحات تخزين الأنابيب واختيار الرافعات الجسرية: الرافعات الشبكية مقابل الصندوقية ومعدات الرفع
تحدد كفاءة مناولة ساحة التخزين الإنتاجية الإجمالية للمصنع. قارن بين الرافعات الجسرية الشبكية والصندوقية، وحلل روافد الرفع لنقل الأنابيب حديثة الفك، وحسّن مسارات التخزين.
عملية إنتاج الأنابيب الخرسانية بأسطوانة التعليق: الدليل الصناعي الشامل خطوة بخطوة
تعد ماكينات أسطوانة التعليق العمود الفقري لإنتاج الأنابيب الخرسانية المسلحة عالية الكثافة (DN300–DN2000). يغطي هذا الدليل تسلسل الإنتاج بالكامل من تدرج الركام ولحام الأقفاص بنظام CNC إلى دمك الأسطوانة والمعالجة بالبخار على 4 مراحل.