Régimen de Curado por Vapor para Tubos de Hormigón: Protocolo Térmico en 4 Etapas
Controle el tiempo de espera, rampa de calentamiento (15°C/h), meseta isotérmica (65–70°C) y enfriamiento para evitar microfisuras.
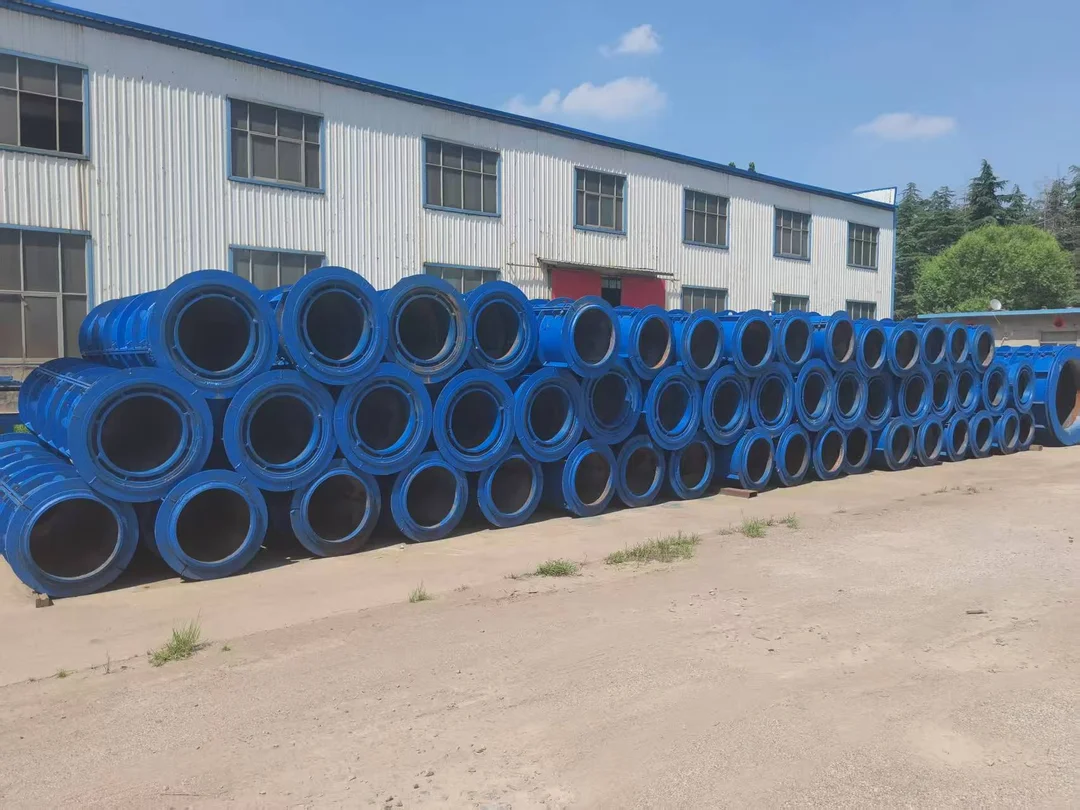
El curado por vapor acelera la resistencia a compresión para un desmoldeo rápido. Aplique nuestro protocolo térmico de 4 fases para alcanzar resistencias de C35 a C50 en 8 horas sin riesgo de fisuración.
1. The Physics of Accelerated Steam Curing
In high-volume precast concrete pipe facilities, waiting 28 days for natural ambient curing before handling or dispatching products is economically impossible. Accelerated atmospheric steam curing (常压蒸汽养护) exposes fresh concrete to saturated steam (relative humidity ≥95%) at elevated temperatures, drastically accelerating calcium-silicate-hydrate (C-S-H) gel formation.
However, cement paste and steel pipe molds possess vastly different thermal expansion coefficients. Rapid, uncontrolled temperature rises cause the trapped water and air within the concrete pores to expand rapidly, rupturing the unformed cement matrix. A strictly monitored 4-stage temperature schedule is essential.
2. The 4-Stage Thermal Schedule in Detail
- 1. Preset Delay Period (静停阶段): The pipe remains inside the curing enclosure with all steam valves shut. This resting phase allows the cement to complete initial setting and develop an early skeletal threshold (penetration resistance ≥3.5 MPa) before thermal expansion begins.
- 2. Controlled Heating Period (升温阶段): Steam is introduced gradually. The rate of temperature increase must not exceed 15°C to 20°C per hour. Temperatures are recorded at 30-minute intervals across multiple sensors.
- 3. Constant Temperature Soaking Period (恒温阶段): Steam flow is modulated to keep chamber temperatures steady at 65°C to 75°C. Variations must be confined within ±5°C. In the event of a steam interruption, the soaking time is extended proportionately using a degree-hour compensation formula.
- 4. Controlled Cooling Period (降温阶段): Steam is closed off. The enclosure cools gradually at a rate not exceeding 15°C to 20°C per hour. When the doors or covers are opened, the temperature differential (ΔT) between the concrete pipe surface and ambient plant air must not exceed 40°C in summer or 30°C in winter.
3. Critical Time & Temperature Parameters
| Curing Stage | Duration (Summer) | Duration (Winter) | Target Temperature | Max Heating/Cooling Rate |
|---|---|---|---|---|
| Preset Delay (静停) | 1.5 – 2.0 hours | 2.0 – 2.5 hours | Ambient (20–25°C) | 0°C (Steam Off) |
| Ramp-Up (升温) | 2.0 – 2.5 hours | 2.5 – 3.0 hours | Rising to 65–75°C | ≤ 20°C / hour strictly |
| Soaking (恒温) | 3.5 – 4.5 hours | 4.0 – 5.5 hours | 65°C – 75°C (±5°C) | Constant hold |
| Cooling (降温) | 1.5 – 2.0 hours | 2.0 – 2.5 hours | Cooling to ≤45°C | ≤ 20°C / hour strictly |
| Total Cycle | 8.5 – 11.0 hours | 10.5 – 13.5 hours | Enables 2 turns / day | Full batch repeatability |
4. Common Curing Failures & Troubleshooting
- Thermal Crazing & Hairline Cracks: Caused by ramping temperatures too rapidly (>20°C/hr) or omitting the preset resting period. Solution: Enforce automatic motorized steam control valves.
- Surface Chalking / Friable Surface: Caused by dry steam or insufficient humidity (<90%). Steam must be saturated wet steam; maintain condensation on mold skins.
- Thermal Shock Fractures: Caused by opening curing doors abruptly into freezing winter air. Solution: Extend natural cooling until surface temperature is within 30°C of ambient.
5. Steam Boiler Sizing & Distribution Design
For a plant operating 2 suspension roller machines and 4 curing pits, a fully automated gas-fired or biomass steam boiler rated for 1.0 to 2.0 tons/hour at 0.7 MPa provides stable, clean saturated steam. Steam delivery headers must feature condensate drain traps and proportional control valves.
6. Demolding Strength Verification
Before lifting the mold to the stripping station, companion test cubes cured in the identical chamber must achieve a compressive strength ≥80% of design strength (typically ≥24–28 MPa). De-molding prematurely risks micro-crack development during crane transport.
Planning a Concrete Pipe Manufacturing Project?
Our engineering team provides comprehensive turnkey plant calculations, foundation layout drawings, mold customization specifications, and commercial quotations within 2 hours.
Artículos Técnicos Relacionados
Mantenimiento de Moldes de Tubos de Hormigón: Alineación de Anillos, Desencofrantes y Desmoldeo
Los moldes de acero son una inversión clave. Maximice su vida útil, mantenga la circularidad de junta en ±0,5 mm y evite desportilladuras con nuestra lista de comprobación de mantenimiento y agentes desencofrantes.
Logística de Patio de Tubos y Selección de Grúas Pórtico: Celosía vs. Cajón y Maniobras Seguras
La logística del parque de almacenamiento marca el rendimiento global de la fábrica. Compare grúas pórtico de celosía frente a viga cajón, analice balancines de elevación y optimice el acopio de tubos recién desmoldeados.
Proceso de Fabricación de Tubos de Hormigón por Rodillo de Suspensión: Guía Industrial Paso a Paso
Las máquinas de rodillo de suspensión son el estándar global para producir tubos de hormigón armado de alta densidad (DN300–DN2000). Esta guía abarca desde la granulometría de áridos y soldadura CNC de jaulas hasta el rodillo de doble velocidad y el curado por vapor en 4 etapas.