Fabricación de Pozos de Registro de Hormigón Prefabricado: Norma ASTM C478 y Bases Monolíticas
Ingeniería de anillos de recrecido, conos excéntricos y bases monolíticas estancas para redes de saneamiento.
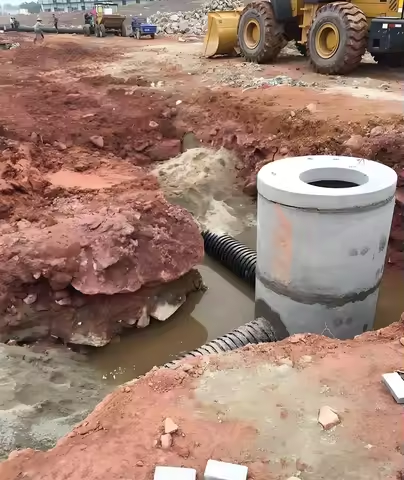
Los pozos de registro prefabricados deben soportar presiones del terreno y evitar la infiltración de agua. Aprenda las configuraciones de moldes para bases, anillos cilíndricos y conos según ASTM C478.
1. The Evolution of Precast Concrete Manhole Systems
In modern underground utility engineering, brick-built inspection wells have been universally banned across major jurisdictions due to chronic mortar joint leakage, root penetration, and high labor costs. Precast reinforced concrete manholes have become mandatory for municipal sanitary sewer, stormwater, electrical, and telecommunication networks.
A complete precast manhole structure must resist heavy AASHTO H-20/HS-20 traffic surface loads, high lateral earth pressures, and corrosive biogenic sulfuric acid attacks while maintaining 100% vacuum watertightness.
2. The 4 Core Manhole Modular Components
HLY supplies complete modular steel tooling sets designed to produce all four critical manhole components:
- Monolithic Base Section (井底座 / Base Invert): Houses the bottom slab and precision-sloped flow channels (benching) with cast-in flexible pipe-to-manhole rubber boots (ASTM C923).
- Riser Sections (井室 / Barrel Risers): Straight cylindrical sections available in standard heights of 250 mm, 500 mm, 750 mm, 1000 mm, and 1500 mm, featuring tongue-and-groove joints.
- Eccentric & Concentric Cones (井筒偏心/同心收口锥体): Reduces the internal chamber diameter (e.g. from DN1000/DN1200 mm down to DN700 mm) to receive standard cast iron manhole frame and cover sets.
- Flat Slab Transition Tops (减缩平板盖板): Heavy reinforced concrete slabs used in shallow burials where conical reducers cannot fit within depth constraints.
3. ASTM C478 & EN 1917 Technical Specifications
ASTM C478 ('Standard Specification for Circular Precast Reinforced Concrete Manhole Sections') establishes rigid dimensional and strength thresholds:
| Component Property | ASTM C478 Requirement | HLY Mold Manufacturing Specification |
|---|---|---|
| Concrete Compressive Strength | Min 27.6 MPa (4,000 psi) at 28 days | Molds designed for C35/C40 (35–40 MPa) mixes |
| Wall Thickness Tolerance | Min 95% of specified wall thickness | CNC turned end rings hold ±2 mm tolerance |
| Internal Diameter Tolerance | ±1% of nominal diameter (e.g., ±10mm on DN1000) | Calibrated to ±3.0 mm across 4 orthogonal axes |
| Joint Mating Gap | Max 5 mm gap with preformed gasket compressed | Machined steel rings ensure gap ≤ 2.5 mm |
| Reinforcement Steel Area | Circumferential rebar per ASTM A1064 | Molds feature integrated rebar spacer slots |
| Vacuum Testing Requirement | Holds 10 in. Hg (-34 kPa) for 60 seconds | Meets ASTM C1244 vacuum acceptance test |
4. Monolithic Base Casting & Integrated Flow Inverts
The base section represents the highest engineering complexity. Two-piece construction (pouring a flat slab and grouting a riser ring on top) creates a vulnerable cold joint prone to severe groundwater infiltration.
HLY monolithic base molds utilize an inverted casting technique with customizable modular core inserts. This allows the factory to cast the bottom slab, riser wall, and curved hydraulic flow channels (inverts) in a single monolithic pour without secondary masonry.
5. Joint Profiles & Resilient Gasket Watertightness
Joint sealing is the primary factor determining sewer system longevity. HLY manhole molds produce precision confined O-ring or profile gasket grooves (ASTM C443):
• Pre-lubricated integrated rubber gaskets (滑动橡胶密封圈) eliminate field contractor errors.
• Butyl rubber flexible mastic rope (ASTM C990) provides dual-layer insurance against hydrostatic head.
6. Production Methods: Wet Cast vs. Dry-Cast Vibration
Depending on client output requirements, HLY molds support two production paradigms:
1. Wet-Cast Self-Consolidating Concrete (SCC): Superior surface aesthetics, ideal for complex multi-pipe connection bases and custom junction chambers.
2. Dry-Cast High-Frequency Core Vibration: High-output vertical casting machine producing a finished riser or cone section every 4 to 6 minutes with immediate mold stripping.
7. Frequently Asked Engineering Questions
Planning a Concrete Pipe Manufacturing Project?
Our engineering team provides comprehensive turnkey plant calculations, foundation layout drawings, mold customization specifications, and commercial quotations within 2 hours.
Artículos Técnicos Relacionados
Soldadura de Jaulas de Acero para Tubos de Hormigón: Fabricación Automatizada y Normas ASTM C76
La resistencia estructural en ensayos de carga D según ASTM C76 depende de la precisión de la jaula. Conozca cómo las soldadoras CNC automatizan la fabricación y eliminan las variaciones del atado manual.
Fabricación de Tubos de Hinca sin Zanja: Resistencia a Alto Empuje, Moldes con Collarín y Norma DIN EN 1916
El microtúnel sin zanja evita cortes en superficie pero somete a los tubos a empujes axiales extremos. Conozca la dosificación de hormigón de alta resistencia, fabricación de moldes con collarín y normas DIN EN 1916.
Proceso de Fabricación de Tubos de Hormigón por Rodillo de Suspensión: Guía Industrial Paso a Paso
Las máquinas de rodillo de suspensión son el estándar global para producir tubos de hormigón armado de alta densidad (DN300–DN2000). Esta guía abarca desde la granulometría de áridos y soldadura CNC de jaulas hasta el rodillo de doble velocidad y el curado por vapor en 4 etapas.