Fabricación de Tubos de Hinca sin Zanja: Resistencia a Alto Empuje, Moldes con Collarín y Norma DIN EN 1916
Ingeniería de tubos de microtúnel con resistencia axial de 1500+ kN, juntas elastoméricas de triple labio y perpendicularidad láser.
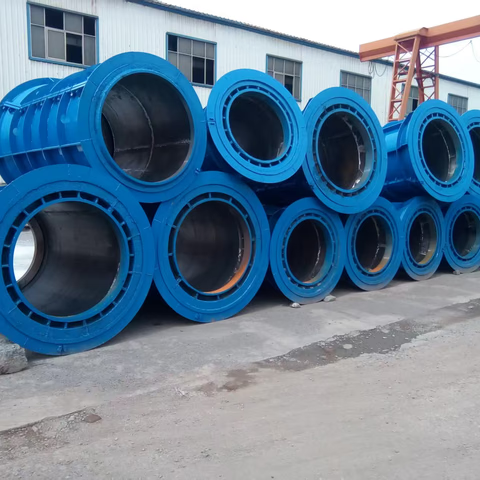
El microtúnel sin zanja evita cortes en superficie pero somete a los tubos a empujes axiales extremos. Conozca la dosificación de hormigón de alta resistencia, fabricación de moldes con collarín y normas DIN EN 1916.
1. The Demanding Physics of Trenchless Pipe Jacking
In modern urban infrastructure, open-cut trench excavation is frequently impossible due to existing highway pavements, building foundations, water bodies, and subterranean metro tunnels. Trenchless pipe jacking (寰《绠?/ 椤惰繘鏂藉伐) propels a cutting shield head underground, with high-capacity hydraulic jacking rams in the drive shaft pushing the string of reinforced concrete pipes forward through the soil.
During driving, each pipe section acts as a structural column transmitting immense axial thrust forces鈥攐ften ranging from 1,500 kN on DN800 pipes to over 12,000 kN on DN2400/DN3000 pipes. Any minute irregularity in end-face squareness will concentrate thrust into point contact, causing catastrophic explosive spalling underground.
2. Jacking Joint Profiles: Steel Collar (F-Type) vs. In-Wall (J-Type)
Two joint architectures dominate international trenchless engineering:
1. Steel Collar Joint (F-Type / 閽㈠鐜帴澶?: A roll-formed Q345B carbon or stainless steel sleeve (thickness 10鈥?6 mm) is cast directly into the spigot end of the pipe. When jacked together, the steel sleeve slides over the adjacent pipe's rebated shoulder, encasing a wedge-shaped elastomeric profile gasket. Offers superior angular deflection tolerance (up to 1.0掳鈥?.5掳) without leaking.
2. In-Wall Rebated Joint (J-Type / 闃舵鎵挎彃鎺ュご): Fully concrete stepped joint with internal rubber gasket groove. Eliminates external steel collars, highly popular in non-aggressive soil environments.
3. Precision End-Ring Tolerances & Lathe Machining
Standard drainage pipe molds allow end squareness deviations of 卤3 mm to 卤5 mm. For jacking pipes, this would cause disastrous point loading under hydraulic ram forces.
| Dimensional Characteristic | DIN EN 1916 / ASTM C76 Jacking Standard | HLY Precision Mold Guarantee |
|---|---|---|
| End Face Perpendicularity | 鈮?1.0 mm deviation across full diameter | 鈮?0.5 mm turned on 8-meter CNC lathe |
| End Face Planarity (Flatness) | 鈮?0.8 mm surface waviness | 鈮?0.3 mm precision ground |
| Pipe Barrel Straightness | 鈮?2.0 mm per meter length (max 4.0 mm) | 鈮?1.0 mm per meter laser verified |
| Steel Collar Recess Fit | Tight tolerance 卤0.5 mm | Interlocking locator pins hold 卤0.3 mm |
| Wall Thickness Uniformity | 卤3 mm around circumference | 卤1.5 mm concentric CNC machined rings |
4. Calculating & Resisting Extreme Axial Thrust Loads
Jacking pipe design must resist permissible jacking force (F_j) calculated per DIN 1610 / ATV-A 161 standards:
F_j 鈮?A_c 脳 f_cd 脳 k_1 脳 k_2
Where A_c is the concrete cross-sectional area, f_cd is the design compressive strength, k_1 accounts for cushion ring stress distribution (0.65鈥?.80), and k_2 accounts for angular deflection during curved driving.
HLY jacking pipe molds ensure the full annular bearing area is 100% planar, maximizing usable thrust capacity without local failure.
5. The Critical Role of Wooden Cushion Packing Rings
Between the concrete pipe faces, a wooden packing cushion ring (鏈ㄥ灚鍦? made from multi-layer marine plywood, chipboard, or fiberboard of 12鈥?8 mm thickness) must be installed. The wooden cushion crushes under early jacking pressure, redistributing uneven stress peaks across the full circumference.
6. High-Performance Concrete Mix: C50/C60 with Silica Fume
Jacking pipes require heavy-duty high-performance concrete (HPC):
鈥?Compressive Strength: Minimum C50 or C60 (50鈥?0 MPa at 28 days; 鈮?5 MPa before demolding).
鈥?Silica Fume / Slag Additions: 5% to 8% condensed silica fume (寰绮? added to refine pore structures, increasing surface abrasion resistance and chemical impermeability against underground slurry.
鈥?Low Water-Binder Ratio: Maintained between 0.30 and 0.34 with high-range polycarboxylate superplasticizers.
7. Frequently Asked Engineering Questions
Planning a Concrete Pipe Manufacturing Project?
Our engineering team provides comprehensive turnkey plant calculations, foundation layout drawings, mold customization specifications, and commercial quotations within 2 hours.
Artículos Técnicos Relacionados
Soldadura de Jaulas de Acero para Tubos de Hormigón: Fabricación Automatizada y Normas ASTM C76
La resistencia estructural en ensayos de carga D según ASTM C76 depende de la precisión de la jaula. Conozca cómo las soldadoras CNC automatizan la fabricación y eliminan las variaciones del atado manual.
Fabricación de Pozos de Registro de Hormigón Prefabricado: Norma ASTM C478 y Bases Monolíticas
Los pozos de registro prefabricados deben soportar presiones del terreno y evitar la infiltración de agua. Aprenda las configuraciones de moldes para bases, anillos cilíndricos y conos según ASTM C478.
Proceso de Fabricación de Tubos de Hormigón por Rodillo de Suspensión: Guía Industrial Paso a Paso
Las máquinas de rodillo de suspensión son el estándar global para producir tubos de hormigón armado de alta densidad (DN300–DN2000). Esta guía abarca desde la granulometría de áridos y soldadura CNC de jaulas hasta el rodillo de doble velocidad y el curado por vapor en 4 etapas.