Производство железобетонных U-образных лотков и каналов: проектирование стальных форм и технология виброформования
Изготовление водоотводных лотков автодорог, мелиоративных каналов и дренажных систем с точными углами распалубки.
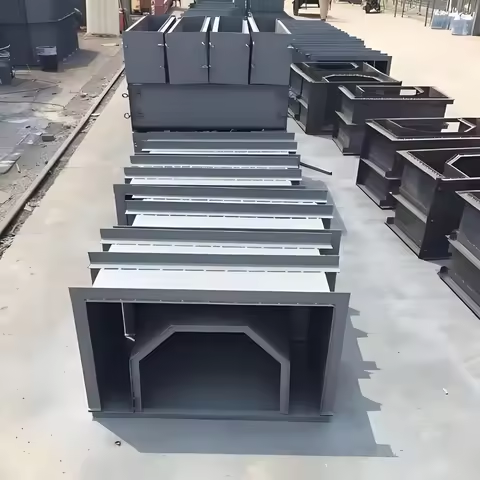
U-образные бетонные лотки требуют строгого соблюдения уклонов распалубки и гладкой гидравлической поверхности. Руководство по расчету стальной опалубки, уплотнению на вибростолах и организации поточного производства.
1. The Crucial Role of Precast U-Channels in Modern Infrastructure
From high-speed railway embankments and highway medians to urban stormwater gutters and agricultural water-saving irrigation networks, precast concrete U-channels (U型槽 / 排水沟) provide superior hydraulic conveyance efficiency compared to unlined earthen ditches or cast-in-place gutters.
Precasting U-channels in factory conditions ensures high compressive strength (C30/C35), low permeability, and glass-smooth hydraulic inverts with a low Manning roughness coefficient (n = 0.012–0.013), minimizing sediment buildup and water delivery losses.
2. Common U-Channel Cross-Sections & Dimensional Classes
HLY manufactures precision steel formwork for a broad spectrum of channel geometries:
- Municipal Drainage Gutters with Cast-Iron Grate Rebates: Standard widths 200–600 mm, depths 200–800 mm, featuring cast-in ductile iron or galvanized steel angle edge protection for traffic load bearing (EN 1433 Class C250 to F900).
- Agricultural Trapezoidal & Semi-Circular Irrigation Flumes: Top widths 600–2000 mm, lengths 2.0–4.0 m, designed for interlocking water-saving irrigation distribution networks.
- Deep Railway Cable & Utility Troughs: Multi-compartment U-channels with matching precast concrete cover slabs.
3. Modular Gang Mold Engineering & Draft Angle Design
Productivity in precast U-channel manufacturing depends upon maximizing output per casting cycle while avoiding surface damage during core withdrawal.
| Design Feature | Standard Fabrication Specification | Operational Advantage |
|---|---|---|
| Gang Mold Configuration | 4 to 8 channel bays per master frame | Multiplies output per crane hoist cycle |
| Demolding Draft Angle (拔模斜度) | 1.5° to 2.5° precision taper on inner core | Prevents surface shear tearing upon stripping |
| Steel Facing Material | 5 mm – 6 mm Q235B cold-rolled steel plate | Zero wave distortion, high wear resistance |
| Hinged Side Formwork | Quick-acting cam-lock levers and hinged wings | Tool-free opening in under 30 seconds |
| Interlocking Joint Profile | Stepped shiplap or tongue-and-groove ends | Ensures precise alignment and mastic sealing |
4. Vibration Consolidation: Table Vibrators vs. Core Poking
Manual poker vibration is inefficient and produces inconsistent concrete density along thin channel walls. HLY recommends two automated consolidation methods:
1. Synchronized High-Frequency Vibration Tables: The complete gang mold is clamped pneumatically to a heavy vibration table operating at 2,800–3,600 rpm. Vibration energy transmits through the entire steel mold, fluidizing low-slump concrete in 45–60 seconds.
2. Formwork-Mounted Pneumatic Vibrators: High-amplitude rotary ball or turbine vibrators mounted symmetrically on the mold frame deliver directional vibration directly to the vertical walls.
5. High-Durability Anti-Scour Concrete Mix Specifications
Because drainage channels and irrigation flumes face continuous water flow, abrasive suspended sand, and freeze-thaw cycles, the concrete mix must achieve:
• Minimum Compressive Strength: C30/C35 (30–35 MPa) at 28 days.
• Water-Cement Ratio: Kept low at 0.36 to 0.40 using polycarboxylate superplasticizers.
• Coarse Aggregate: Crushed basalt or granite (max size 10–15 mm, graded) to resist water scour.
• Air Content: 4.0% to 5.5% air entrainment for cold climates subject to winter de-icing salts.
6. Demolding Cycles, Grate Seating & Storage Yard Handling
With accelerated steam curing or radiant heat beds, U-channel gang molds complete 2 to 3 turnover cycles per 8-hour shift. Precast units are hoisted using specialized scissor clamps or lifting threaded sockets cast into the channel walls.
Channels are palletized horizontally with timber battens between tiers (maximum 5 tiers high), ready for immediate flatbed container loading.
7. Frequently Asked Engineering Questions
Planning a Concrete Pipe Manufacturing Project?
Our engineering team provides comprehensive turnkey plant calculations, foundation layout drawings, mold customization specifications, and commercial quotations within 2 hours.
Связанные технические руководства
Радиальное прессование или виброформование с сердечником: выбор оборудования для завода ЖБИ
Выбор между роликовым радиальным прессованием и вертикальным виброформованием с выдвижным сердечником определяет бюджет оснастки и сменный выпуск труб. Анализируем динамику уплотнения, штат рабочих и окупаемость.
Двухвальные бетоносмесители для трубных производств: механика перемешивания жестких смесей JS500–JS1500
Жесткие бетонные смеси требуют колоссальной энергии сдвига для равномерного распределения цементного теста. Руководство по эксплуатации двухвальных смесителей серии JS, контролю влажности смеси и защите брони от абразивного износа.
Производство железобетонных труб радиальным прессованием: пошаговое руководство для заводов ЖБИ
Станки радиального прессования — мировой стандарт для выпуска безнапорных железобетонных труб (DN300–DN2000). В руководстве подробно описан весь технологический цикл: от гранулометрии песка и щебня до двухскоростной прикатки и пропарки в ямных камерах.