Радиальное прессование или виброформование с сердечником: выбор оборудования для завода ЖБИ
Сравнение производительности, затрат на металлоформы, требований к жесткости бетона и точности раструбного стыка.
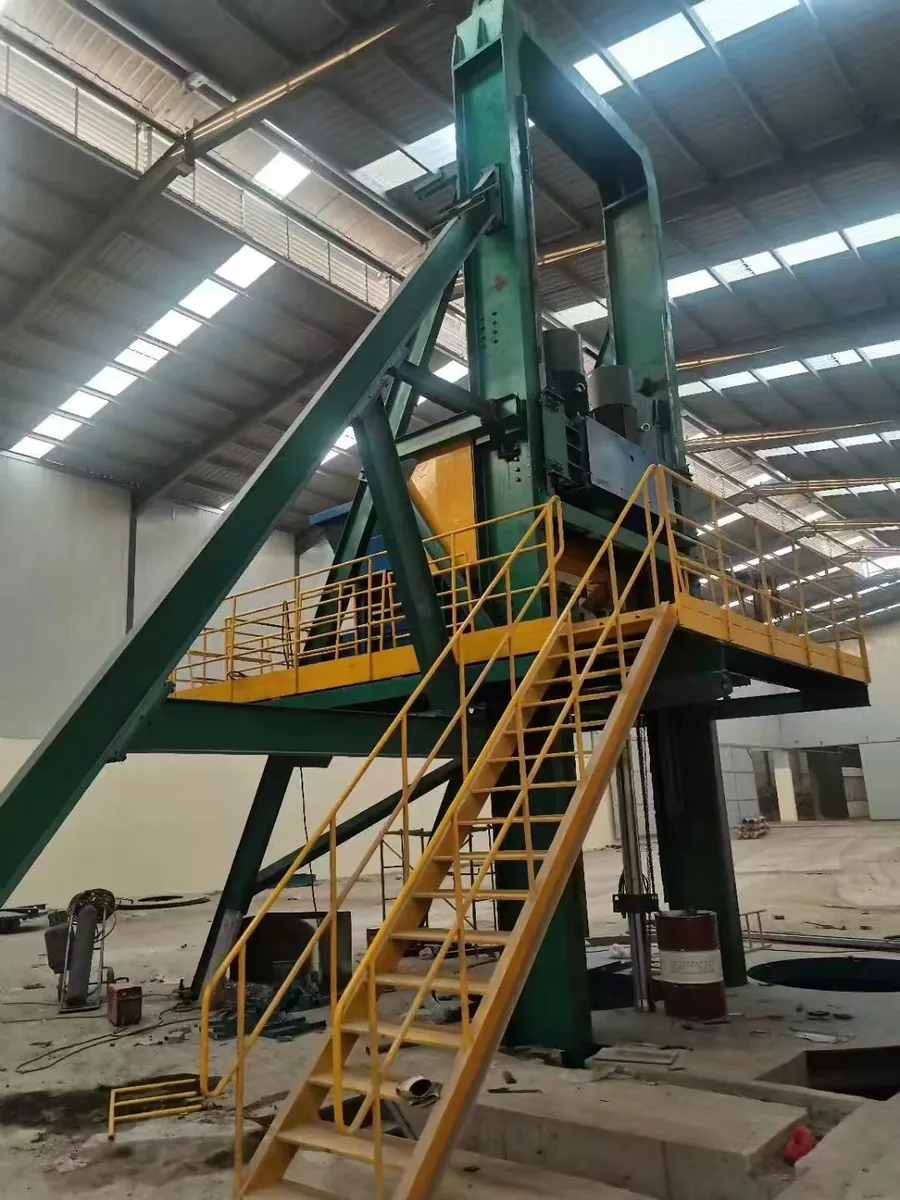
Выбор между роликовым радиальным прессованием и вертикальным виброформованием с выдвижным сердечником определяет бюджет оснастки и сменный выпуск труб. Анализируем динамику уплотнения, штат рабочих и окупаемость.
1. The Technology Dilemma in Precast Concrete
Investors and plant managers establishing or expanding reinforced concrete pipe (RCC) manufacturing plants universally face one central decision: Should the facility install horizontal suspension roller compaction machinery, or invest in automated vertical rising-core vibration lines?
While both systems produce heavy-duty concrete pipes conforming to ASTM C76, BS 5911, and DIN EN 1916, their capital expenditure structure, mold requirements, floor space footprint, and operational flexibility diverge dramatically.
2. Working Principles & Forming Mechanics
Suspension Roller Machine: Operates horizontally. The pipe mold rests on a heavy roller shaft driven by an inverter motor. Dry-cast concrete is introduced via a feed conveyor. Centrifugal force holds the concrete against the mold circumference, while high line pressure from the roller shaft crushes and compacts the mix.
Vertical Rising-Core Vibration Machine: Operates vertically. The mold consists of an outer steel jacket, a bottom pallet ring, and a motorized internal core equipped with high-frequency hydraulic vibrators. Zero-slump dry concrete is fed from the top while the core vibrates at 3,000–4,500 rpm. Once compacted, the inner core automatically rises out, allowing immediate demolding of the outer mold within 3 to 5 minutes.
3. Direct Technical Comparison Matrix
| Engineering Criteria | Suspension Roller Line | Vertical Rising-Core Vibration |
|---|---|---|
| Diameter Range | DN300 – DN2000 mm | DN600 – DN3000 mm (up to DN3500) |
| Standard Pipe Length | 2.0 m, 2.5 m, 3.0 m, 4.0 m | 2.5 m, 3.0 m, 3.5 m |
| Demolding Speed | Requires steam curing before demolding (3–5 hr in mold) | Immediate demolding (3–5 minutes per pipe) |
| Mold Quantity Needed | 1 mold required per pipe produced per shift (e.g., 20–40 molds) | Only 1 outer mold needed per size + multiple bottom pallets |
| Initial Machine Cost | Moderate (Low entry barrier) | Higher (Advanced hydraulic/PLC systems) |
| Total Mold Investment | High when producing high daily volumes | Very Low (Only buy bottom pallets for volume) |
| Concrete Slump | Dry-cast (Vebe 20–30s) | Zero-slump (Dry-cast, high vibration liquefaction) |
| Labor Requirement | 2–3 operators per line | 3–4 operators per plant |
| Internal Surface Finish | Extremely smooth (Polished by spinning roller) | Smooth, dense vibrated surface |
| Jacking Pipe Production | Excellent up to DN2000 | Superior for large DN1200–DN3000 heavy jacking pipes |
4. Mold Economics & Capex Footprint
The greatest financial difference lies in mold expenditure. In a suspension roller facility producing 40 pipes per 8-hour shift, the plant must purchase and maintain 40 complete steel pipe molds, because the pipe must remain inside its mold throughout the initial steam curing cycle.
Conversely, a vertical rising-core vibration plant utilizes immediate dry-cast demolding. The single outer mold is stripped immediately after compaction and reused for the next pipe. The plant only requires inexpensive base pallet rings (底托盘) to support the curing pipes. For large pipe sizes (e.g., DN1500–DN3000), where individual steel molds can cost $8,000–$18,000 each, the vertical vibration line generates tremendous capital savings.
5. Production Output, Cycle Times & Labor
Cycle Times: A suspension roller machine requires 8–15 minutes of active rolling per pipe, producing 30–50 pipes per shift. A vertical rising-core system achieves complete feed, vibration, and core-stripping in 4–7 minutes, delivering 60–80 pipes per shift with automated batching.
Floor Space: Suspension roller plants require extensive horizontal trackways, gantry crane spans, and mold handling areas. Vertical plants require greater vertical building clearance (typically 10–12 meters hook height) but occupy a more compact ground footprint.
6. Ideal Application Scenarios for Each System
- Choose Suspension Roller When: Your target market demands high volumes of small to mid-diameter drainage and culvert pipes (DN300–DN1200); capital budget is focused on lean startup; your plant already has horizontal steam curing tunnels.
- Choose Vertical Rising-Core When: Your primary contracts involve large-diameter municipal storm sewers (DN1000–DN3000) or microtunneling trenchless jacking pipes; high daily output is required without storing dozens of massive steel molds; you want a modern, fully enclosed automated plant.
7. Engineering Recommendation & Decision Matrix
For new turnkey precast facilities entering infrastructure markets, the optimal configuration frequently combines both systems: a suspension roller line to handle high-velocity DN300–DN1000 culvert pipe orders, paired with a vertical rising-core station dedicated to large-diameter DN1200–DN3000 jacking and sewer infrastructure.
Planning a Concrete Pipe Manufacturing Project?
Our engineering team provides comprehensive turnkey plant calculations, foundation layout drawings, mold customization specifications, and commercial quotations within 2 hours.
Связанные технические руководства
Производство железобетонных U-образных лотков и каналов: проектирование стальных форм и технология виброформования
U-образные бетонные лотки требуют строгого соблюдения уклонов распалубки и гладкой гидравлической поверхности. Руководство по расчету стальной опалубки, уплотнению на вибростолах и организации поточного производства.
Двухвальные бетоносмесители для трубных производств: механика перемешивания жестких смесей JS500–JS1500
Жесткие бетонные смеси требуют колоссальной энергии сдвига для равномерного распределения цементного теста. Руководство по эксплуатации двухвальных смесителей серии JS, контролю влажности смеси и защите брони от абразивного износа.
Производство железобетонных труб радиальным прессованием: пошаговое руководство для заводов ЖБИ
Станки радиального прессования — мировой стандарт для выпуска безнапорных железобетонных труб (DN300–DN2000). В руководстве подробно описан весь технологический цикл: от гранулометрии песка и щебня до двухскоростной прикатки и пропарки в ямных камерах.